

 English
 中文简体
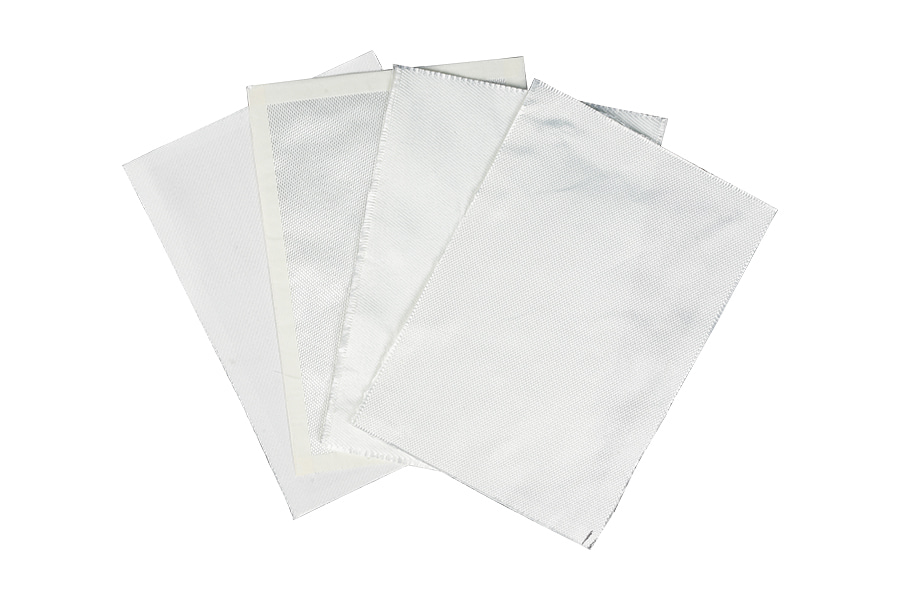
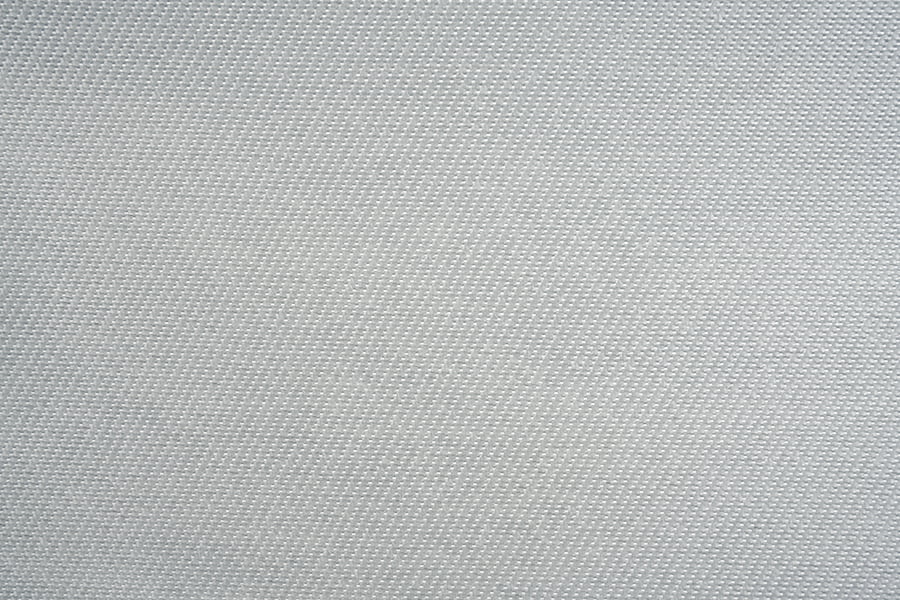

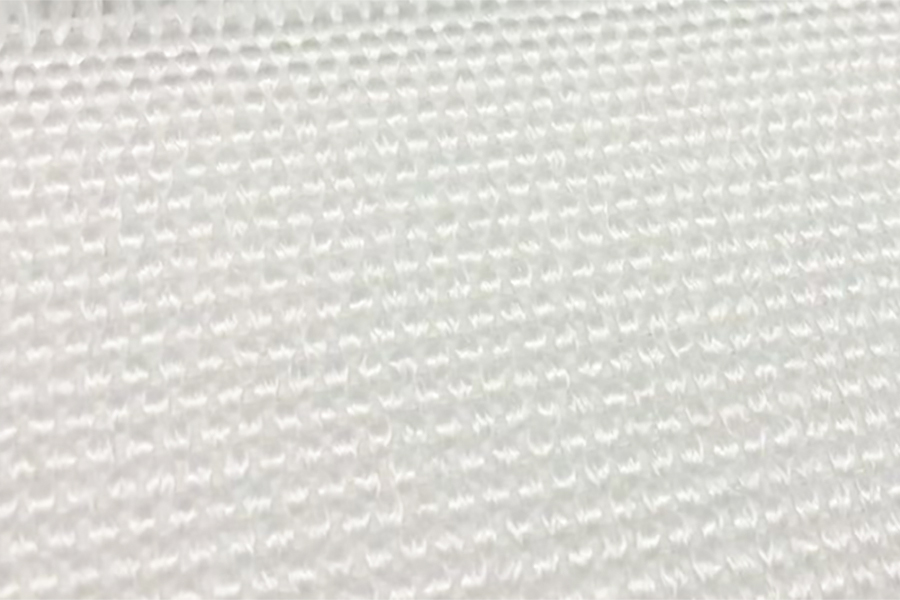
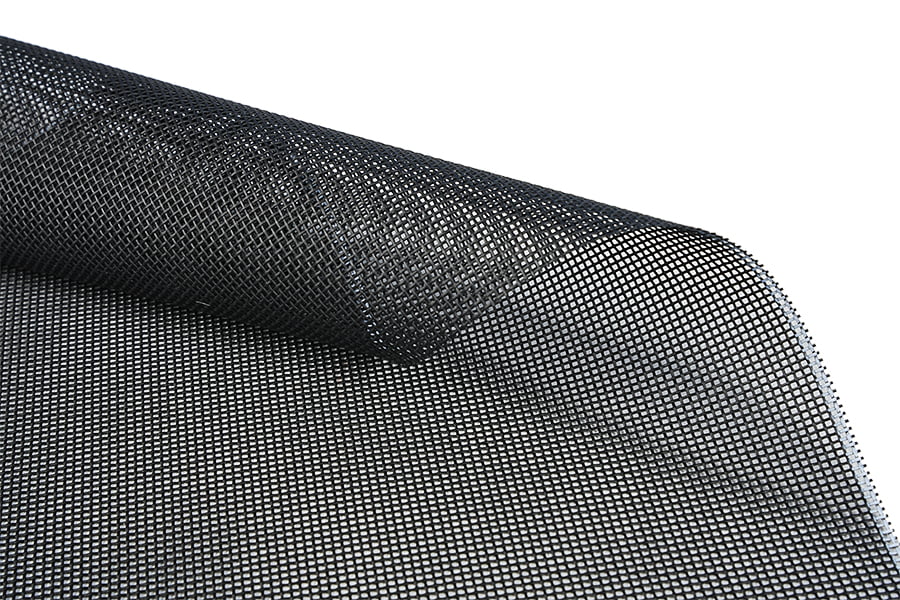
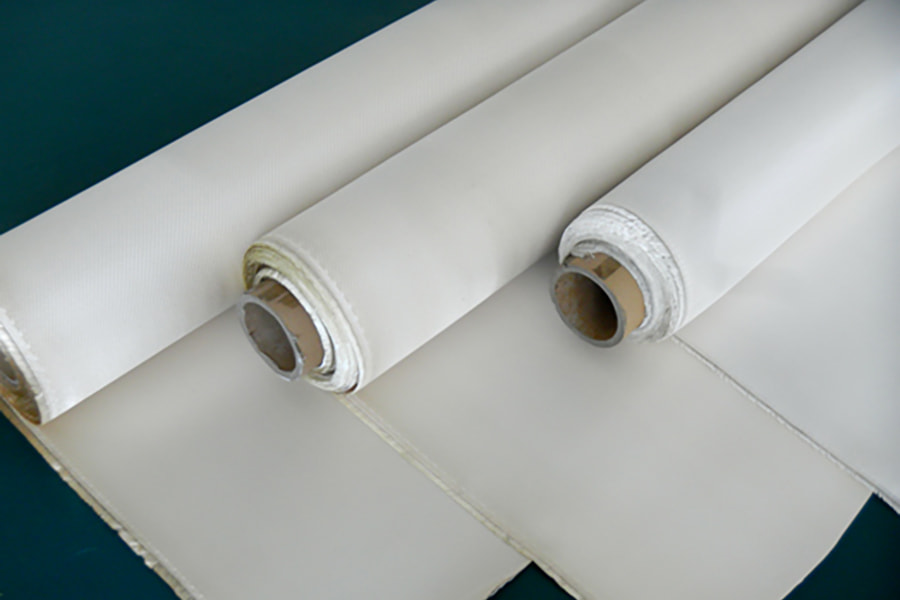
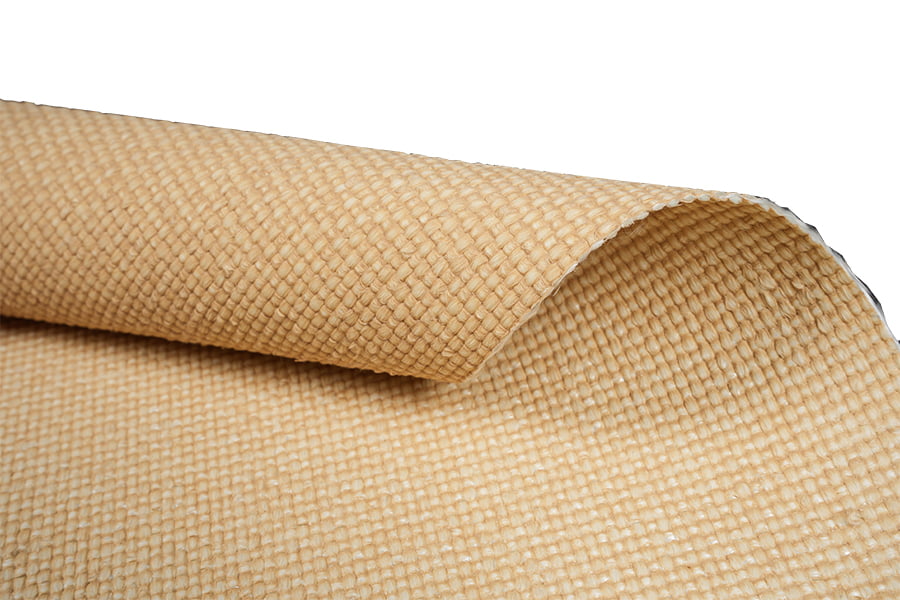
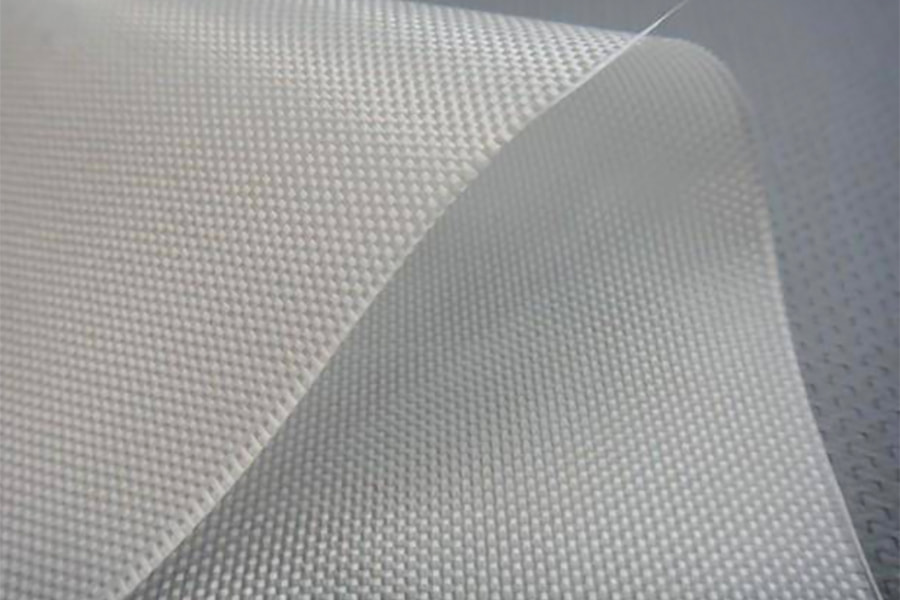
fine weave fiberglass cloth
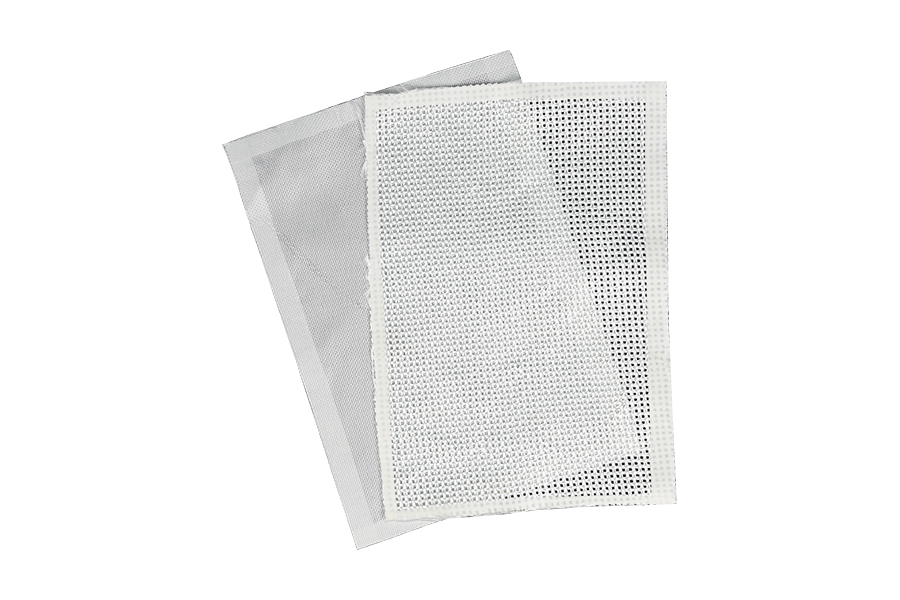
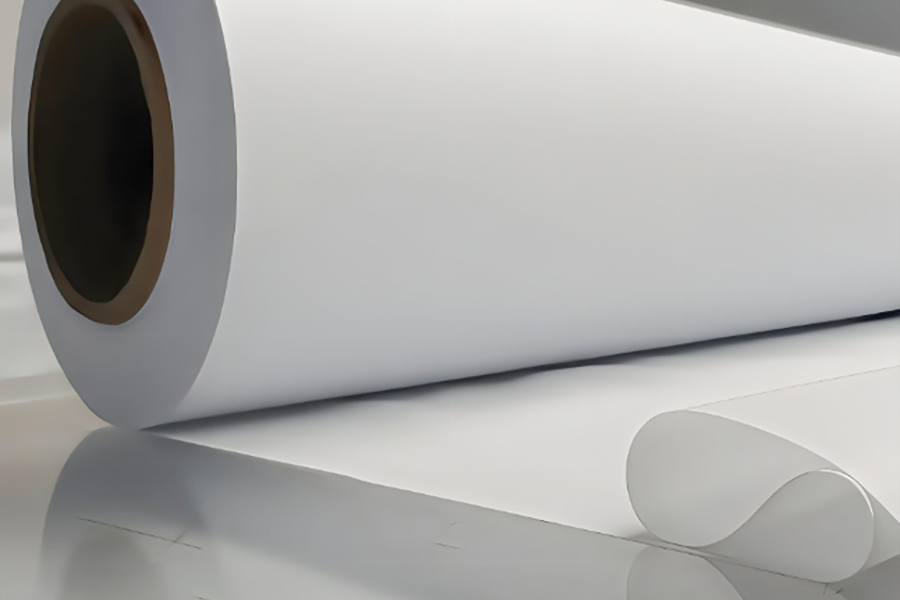
Fine weave fiberglass cloth is produced from low tex E-glass yarns with a high yarn count per unit width, resulting in a tightly interlaced fabric with a thin cross-section and a smooth surface profile. The fine yarn architecture reduces surface texture amplitude and improves mechanical translation in thin laminates. The fabric is supplied in areal weights from 25 g/m² to 200 g/m² and thicknesses from 0.03 mm to 0.20 mm, with tensile strength from 150 MPa to 320 MPa depending on construction. Fine weave fiberglass cloth is compatible with epoxy, polyester, vinylester, and phenolic resins and is used where surface finish, resin control, or thin section reinforcement is the primary requirement. Roll widths from 1000 mm to 1500 mm and roll lengths from 50 m to 300 m are standard.
Construction Data
Surface Grade Finish
Fine yarns reduce the amplitude of the weave pattern on the laminate surface. Print-through in gelcoat and paint is minimized compared with standard weave fabric at equal weight, reducing sanding and finishing labor in visible-surface applications.
Thin Section Control
Low thickness per ply supports precise laminate buildup in thin skins, surfacing layers, and structural inserts where total thickness tolerance is tight. Fine weave also reduces resin pooling in sharp radii and tight corners.
Rapid Wet-out
Small yarn cross-section accelerates resin penetration and reduces void content in thin laminates. Complete wet-out is typically achieved within seconds under vacuum, supporting short cycle times in infusion and RTM processes.
Dimensional Stability
High interlacement density limits yarn movement during cutting and lay-up. The fine weave holds ply geometry on complex contours and reduces edge fraying compared with coarse weave at equivalent weight.
Qualified Verticals
Production Notes
Fine weave holds its shape well during cutting with minimal fraying. Use sharp rotary cutters or shears. For high volumes, laser or ultrasonic cutting reduces edge deformation.
Low bending stiffness supports conformability to compound curves and tight radii. Avoid over-stretching on complex molds, which can distort the fine weave pattern and cause local resin-rich zones.
Fast wet-out supports short infusion cycles. For vacuum infusion, use resin viscosity of 150 to 300 cP at 25°C and verify fill time on trial panels. Avoid excessive flow medium, which can cause resin pooling under the thin fabric.
Store rolls horizontally at 15 to 30°C and 40 to 60 percent RH. Keep rolls wrapped to protect the fine yarns from dust and mechanical damage. Shelf life is 36 months in original packaging.
Procurement and Engineering FAQ
Fine weave uses low tex yarns with a higher yarn count, producing lower surface texture amplitude than standard weave at equal weight. This reduces print-through in gelcoat and paint, cutting the sanding and filling labor required to reach a Class-A finish. The trade-off is lower mechanical strength per ply and higher material cost per unit weight.
Fine weave is generally used as a surfacing ply or in thin laminates where thickness control and surface finish are the primary requirements. For structural loads, it is combined with heavier fabric such as twill or plain weave. Multiple plies of fine weave can be stacked for moderate structural buildup, but the total number of plies increases compared with heavier fabric at equal thickness.
Standard MOQ is 200 kg per width and weight specification. Stock widths of 1000 mm and 1270 mm in the 25 to 100 g/m² range ship from inventory within 5 to 10 business days. Lighter weights, wider rolls, and custom sizing systems typically require 3 to 5 weeks depending on order volume.
Yes. Fine weave wet-out is rapid due to the small yarn cross-section. Use resin viscosity of 150 to 300 cP at 25°C. For large parts, confirm flow balance on trial panels because the fine weave can wick resin unevenly if flow media is placed incorrectly. Debulk every three to four plies in thicker buildups.
Each shipment includes a certificate of analysis covering areal weight, thickness, yarn count, sizing system, and roll length. Lot numbers are recorded for traceability. Additional test data including tensile strength and resin compatibility statements can be provided on request for qualified accounts.